Encapsulation & Blending Solutions Supplier Since 2003
Encapsulation & Blending Solutions Supplier Since 2003
| Core Content | Standard 85%, customizable |
|---|---|
| Wall Material | Lipids, dextrin, emulsifiers, or salts (customizable) |
| Packaging | 25 kg bags, customizable packaging available |
| MOQ | 200 kg / 500 kg (customized orders) |
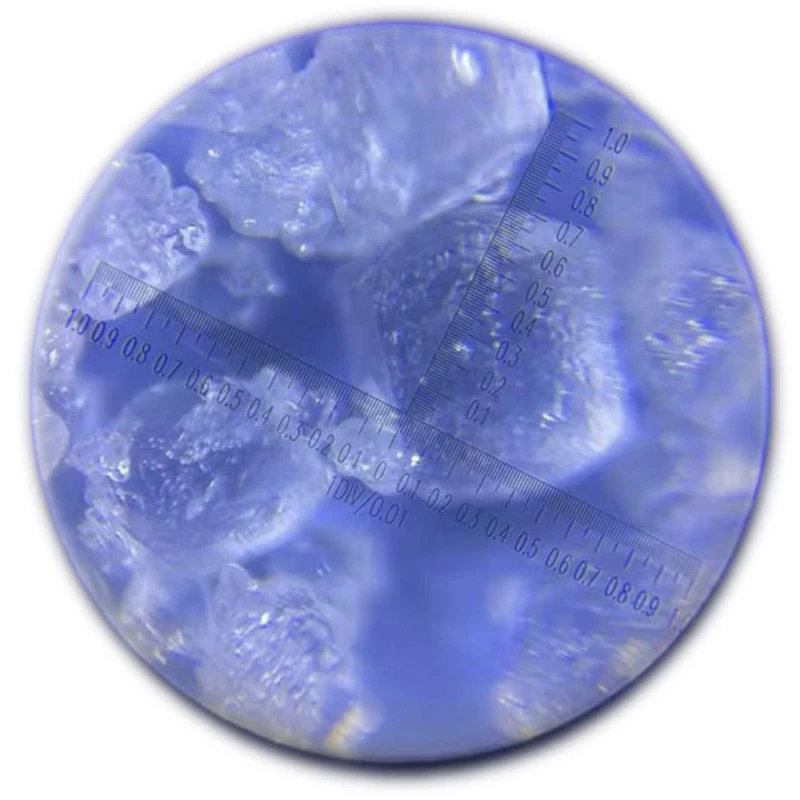
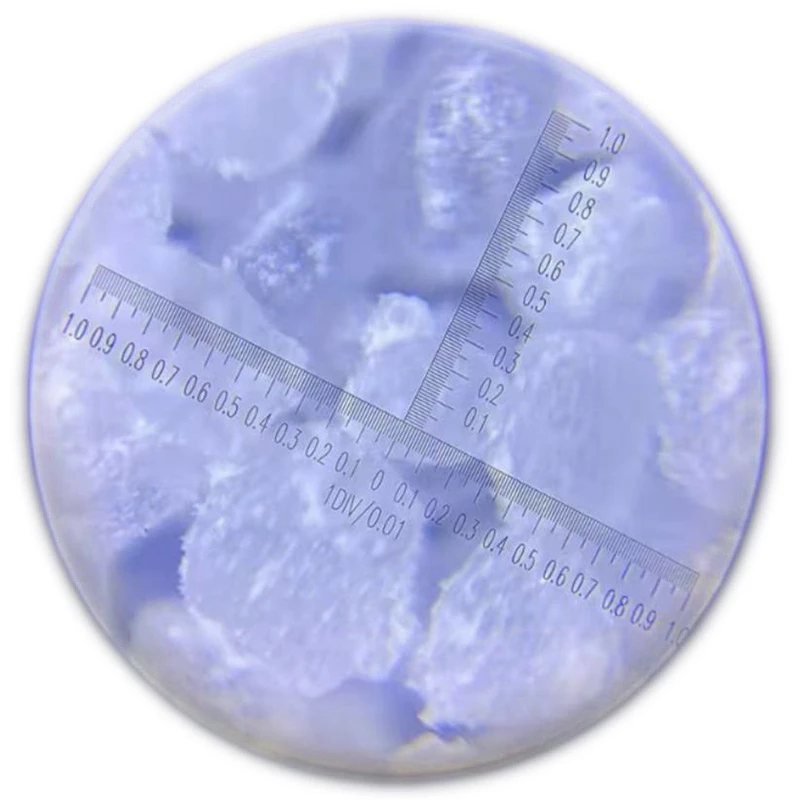
Encapsulated Ascorbic Acid (Vitamin C) is an advanced controlled-release antioxidant and nutrient stabilizer produced using state-of-the-art microencapsulation technology. High-purity ascorbic acid crystals are coated with a food-grade protective layer, available in both hydrophilic (water-soluble wall material) and hydrophobic (lipid or wax-based coating) variants. Both types remain stable at room temperature, significantly reducing interaction with moisture, oxygen, light, and other reactive components. The active ingredient is released only under specific trigger conditions.
This technology effectively addresses common limitations of regular ascorbic acid, including high sensitivity to oxidation, rapid degradation during processing, premature interaction with other ingredients, and loss of functional activity. It delivers a more stable, efficient, and reliable solution for antioxidant protection and vitamin fortification. It helps preserve nutritional value, extend shelf life, and maintain consistent product performance in demanding processing environments.
It is widely used as a controlled release antioxidant and vitamin C source in applications where maintaining nutrient stability, preventing oxidation, and ensuring consistent product performance are critical, including beverages, bakery products, functional foods, dietary supplements, and pharmaceutical formulations.
Encapsulated Ascorbic Acid is available in two controlled-release systems, designed to meet different processing and application requirements.
Encapsulated Ascorbic Acid offers significant functional and processing advantages compared to regular ascorbic acid, especially in applications requiring improved oxidation stability, nutrient protection, and controlled release performance.
Encapsulated Ascorbic Acid is widely used in applications requiring improved oxidation stability, nutrient protection, and controlled release performance.
| Item | Specification | Remarks |
| Wall Material | Lipids, dextrin, emulsifiers, or salts | Custom combinations available |
| Core/Wall Ratio | 60–90% core / 10–40% wall | Flexible adjustment |
| Encapsulation Efficiency | ≥97% | High utilization, minimal loss |
| Particle Size | 25–60 mesh | Customizable |


We connect you with the right manufacturers based on your pricing and specification needs.
Diversified supply channels ensure consistent availability and reduce supply risks.
Optimized sourcing strategy helps provide competitive pricing for bulk orders.
Serving clients in over 100 countries with reliable logistics and documentation support.
Fast quotation and professional support for food, beverage, and industrial applications.
Sourced from certified manufacturers, meeting ISO, FSSC 22000, Halal, and Kosher standards.
What is the difference between encapsulated ascorbic acid and regular ascorbic acid?
Regular ascorbic acid is highly sensitive to oxygen, light, and moisture, leading to rapid degradation and loss of activity during processing and storage. Encapsulated ascorbic acid provides controlled release under specific moisture or temperature conditions, protecting the active ingredient and ensuring better stability and effectiveness.
How does encapsulation improve the stability of vitamin C during storage?
The protective coating shields ascorbic acid from oxygen, moisture, and light, significantly slowing down oxidation and degradation. This helps maintain higher vitamin activity over extended storage periods compared to regular ascorbic acid.
What applications is encapsulated ascorbic acid suitable for?
It is widely used in beverages, bakery products, confectionery, seasonings, dietary supplements, and pharmaceutical applications where improved oxidation stability, nutrient protection, and controlled release are required.
Can the product be customized to our specific process?
Yes. We offer full customization of particle size, core-to-wall ratio, coating type, and release profile to match different processing conditions and product requirements. Samples are available for testing.
How do I select the release temperature?
Standard release temperature ranges are available and can be tailored based on your production process, such as baking, extrusion, or beverage processing conditions.
What are the advantages of encapsulated ascorbic acid in production?
It improves oxidation stability, prevents premature degradation, enhances process stability, and maintains consistent nutritional value and product quality, especially in high-temperature or oxygen-sensitive formulations.
How can I obtain samples and technical support?
Contact our team for sample requests and technical guidance. We provide formulation support to help optimize performance in your specific application.
Submit your inquiry to receive a quotation within 24 hours.
WhatsApp us